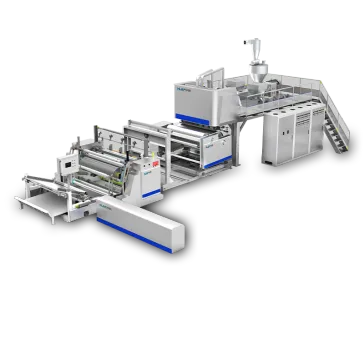
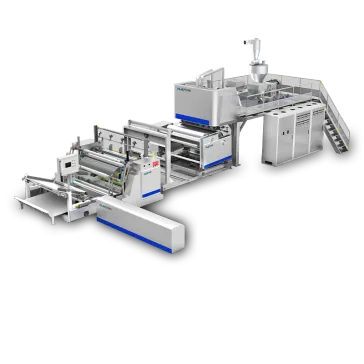
High-Efficiency 3-Layer Cast Film Extrusion Machinery

Description
Core Structural Efficiency: Advanced ABC Co-Extrusion Architecture
Engineered for industrial-scale high-performance packaging, our 3-layer co-extrusion technology establishes an optimal balance between resin economy and film durability. The specialized ABC layer distribution isolates specific mechanical functions across three distinct channels:
- Outer Layer (A): Formulated for high cling and surface adhesion to secure palletized loads without film migration.
- Core Layer (B): Utilizes specialized LLDPE, metallocene (mLLDPE), or up to 20% post-consumer/post-industrial recycled (PCR/PIR) resin, reducing raw material costs by 15–20% without compromising structural integrity.
- Inner Layer (C): Delivers ultimate puncture, tear, and tensile strength to withstand sharp-edged cargo corners.
- Compared to traditional 2-layer films, this strategic resin allocation increases puncture resistance by 30–50% at equivalent thickness, ensuring reliable containment for demanding export packaging.
Thermal Precision & Continuous Melt Homogeneity
To maintain tight thickness tolerances across high-speed production runs, the 3-layer line integrates three independent extrusion units operating within a precisely controlled thermal window of 180°C to 240°C:
- Optimized Screw Geometry: Features a 33:1 L/D ratio with specialized barrier mixing elements, eliminating un-melted gels and temperature fluctuations.
- Precision T-Die & Distributor Block: Ensures smooth layer bonding with a die-lip gap precision within ±0.01mm, minimizing gauge deviation across the effective film width.
- Rapid Thermal Stabilization: A large-diameter primary chill roll rapidly quenches the molten extrudate to maintain exceptional optical clarity and lock in amorphous film stretchability.
Closed-Loop Quality Control & 350% Pre-Stretch Performance
Operating efficiency is reinforced through integrated inline measurement and tension automation:
- Inline Gauge Control: Closed-loop X-ray or infrared scanning sensors continuously monitor film profile, transmitting real-time feedback to auto-adjust die bolts and extruder throughput.
- High-Ratio Traction Unit: Precision speed-synchronized stretching rollers impart a stable pre-stretch capability exceeding 350%, drastically reducing film consumption per wrapped pallet.
- Inline Trim Reclamation & Continuous Winding: Edge trims are directly re-fed into Extruder B via integrated recycling units, while the non-stop turret winder guarantees uniform, wrinkle-free roll profile under continuous operation.
Heavy-Duty Applications & Industrial Compliance
Designed to meet rigorous supply chain demands, the film produced by this system excels in:
- Industrial logistics consolidation and heavy-duty pallet wrap.
- Sharp-edge building materials, ceramic tiles, and machinery packaging.
- Moisture-barrier protection and long-haul export shipping.
- Manufactured under strict engineering standards with CE safety compliance, providing packaging converters with verifiable operational reliability and high ROI.
Quick Comparison: 2-Layer vs 3-Layer Stretch Film
| Parameter | 2-Layer Film | 3-Layer Film |
|---|---|---|
| Structure | AB (cling + strength) | ABC (strength + toughening + cling) |
| Puncture Resistance | Standard (baseline level) | 30–50% higher |
| Max Stretch Ratio | 200–300% | 300–400% |
| Raw Material Cost | Standard (baseline level) | 15–20% lower (middle layer can use recycled material) |
| Film Performance | Basic protection for general use | Enhanced durability and load stability |
| Best Application | Light, regular-shaped loads | Heavy, irregular, high-demand loads |
Applications

Application of 3-Layer Stretch Film Manufacturing Machine in...


Specifications
| Specification | HLCPE75/55-1000 | HLCPE90/65/65-1500 | HLCPE120/80/80-2000 | Unit |
|---|---|---|---|---|
| Product Width | 500-1000 | 1500(500×3rolls) | 2000(500×4rolls) | mm |
| Output | 80 | 320 | 400-600 | kg/hr |
| Product Thickness | 0.01-0.05 | 0.01-0.05 | 0.01-0.05 | mm |
| Mechanical Design Line Speed | 80 | 250 | 250 | m/min |
| L/D | 33:1 | 33:1 | 33:1 | |
| Screw Diameter | φ75/φ55 | φ90/φ65/φ65 | φ120/φ80/φ80 | mm |
| Total Power | 110 | 150 | 350 | kw |
| Power Supply | 380/3/4/50 | 380/3/4/50 | 380/3/4/50 | Volt/Ph/Line/Hz |
| Motor Power | 30/18.5 | 50/22/22 | 132/37/37 | kw |
| Overall Dimensions | 10439*4140*2939 | 14000×6500×4500 | 14000×6500×5000 | (L×W×H)mm |
Product Comparison
 Comparison Item
Ordinary T-Die features low processing precision (tolerance > 0.05 mm) and hardness below HRC45. They are prone to wear and deformation, resulting in uneven film thickness.
Using JC-TIMES high-precision T-DIE, the die lip gap tolerance is controlled within ±0.01mm, and the nitriding hardness reaches HRC ≥ 58, ensuring uniform and stable film thickness.
Ordinary chains have a cumulative error of more than 0.5 mm, require regular lubrication, and their vibration causes convex ribs on the film roll.
Hualiang timing belt delivers zero-error transmission synchronization, requires no lubrication or maintenance, operates at a noise level of less than 65 dB, and ensures the film roll is perfectly smooth and flawless.
Thin-Walled Barrels: Rapid heat dissipation requires constant reheating, resulting in 25–30% higher energy waste. Temperature Fluctuations: lead to uneven melting and thickness variations (±8–10%).
Thick-Walled Barrel: Enhanced thermal retention minimizes heat loss, reducing power consumption by 15–20% compared to thin-walled barrels. Uniform Melt Temperature: Maintains stability within ±5°C, ensuring consistent bubble formation and achieving a thickness tolerance of ±3%.
Asynchronous motors feature higher operational inertia and an IE2 efficiency of 94.2%.
The Permanent Magnet Synchronous Motor (PMSM) reduces energy consumption by 20%, delivers torque control accuracy of ±1%, and enables instant start-stop response.
Conventional heating coils feature slow heating, inadequate insulation, and high power consumption.
Hualiang Infrared Heating System boosts thermal efficiency by 40% and reduces overall energy consumption by 20%.
Ordinary T-Die features low processing precision (tolerance > 0.05 mm) and hardness below HRC45. They are prone to wear and deformation, resulting in uneven film thickness.
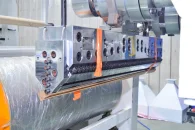
Using JC-TIMES high-precision T-DIE, the die lip gap tolerance is controlled within ±0.01mm, and the nitriding hardness reaches HRC ≥ 58, ensuring uniform and stable film thickness.
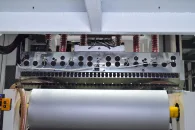
Ordinary chains have a cumulative error of more than 0.5 mm, require regular lubrication, and their vibration causes convex ribs on the film roll.
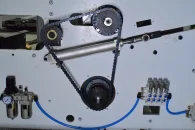
Hualiang timing belt delivers zero-error transmission synchronization, requires no lubrication or maintenance, operates at a noise level of less than 65 dB, and ensures the film roll is perfectly smooth and flawless.
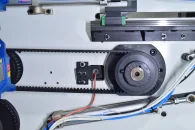
Thin-Walled Barrels: Rapid heat dissipation requires constant reheating, resulting in 25–30% higher energy waste. Temperature Fluctuations: lead to uneven melting and thickness variations (±8–10%).
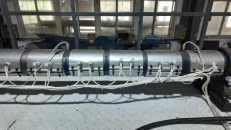
Thick-Walled Barrel: Enhanced thermal retention minimizes heat loss, reducing power consumption by 15–20% compared to thin-walled barrels. Uniform Melt Temperature: Maintains stability within ±5°C, ensuring consistent bubble formation and achieving a thickness tolerance of ±3%.
Asynchronous motors feature higher operational inertia and an IE2 efficiency of 94.2%.
The Permanent Magnet Synchronous Motor (PMSM) reduces energy consumption by 20%, delivers torque control accuracy of ±1%, and enables instant start-stop response.
Conventional heating coils feature slow heating, inadequate insulation, and high power consumption.
Hualiang Infrared Heating System boosts thermal efficiency by 40% and reduces overall energy consumption by 20%.


Others


 GET IN TOUCH NOW

Custom Service
We offer all-round customization for packaging machinery, covering exclusive configurations, diverse styles and personalized sizes. We tailor professional solutions to meet your wholesale, bulk and brand ordering demands.


